


 Home
Ultrasonic Wire Splice vs Soldering vs Crimping: A Buyer's Guide | Borude
September. 15,2026
Choosing the right electrical connection process directly affects warranty costs, production throughput and field reliability. For engineers sourcing equipment for automotive harnesses, appliance wiring or energy storage systems, the debate usually narrows to three options: soldering, crimping and ultrasonic wire splice welding. This guide compares all three from a purchasing perspective and explains why more OEMs are switching to Borude ultrasonic metal welders.
Why the Connection Method Matters
Every joint in a wire harness is a potential failure point. Vibration, thermal cycling, moisture and high current can turn a weak connection into a warranty claim. Soldering has been the default for decades, crimping dominates high-volume automotive lines, and ultrasonic wire splicing is now the preferred choice where low resistance, high mechanical strength and process repeatability are non-negotiable.
Buyers should evaluate a joining technology on four axes: electrical performance, mechanical durability, cycle economics and environmental compliance. The following sections break each method down against those criteria.

Borude ultrasonic wire splice welder designed for copper and aluminum stranded conductors
How Ultrasonic Wire Splicing Works
Ultrasonic wire splicing uses high-frequency mechanical vibration (typically 20 kHz) combined with controlled clamping pressure. The vibration scrubs surface oxides away, raises the metal temperature through friction, and creates a solid-state metallurgical bond without melting the conductor. Because the base metal never reaches its melting point, the weld zone retains nearly the same conductivity and tensile strength as the parent wire.
Borude ultrasonic splicers add closed-loop amplitude and force feedback, so every joint is produced within a tight process window. No flux, solder paste or consumable electrodes are required, which simplifies supply chains and eliminates the risk of corrosive residues.
Head-to-Head: Soldering vs Crimping vs Ultrasonic Splicing
| Criterion | Soldering | Crimping | Ultrasonic Splicing |
|---|---|---|---|
| Joint resistance | Higher due to solder alloy | Variable, depends on terminal quality | Near-parent metal, very low |
| Mechanical strength | Moderate, brittle at low temps | Good under static load | High tensile and vibration resistance |
| Heat input | High, can anneal copper | None | Localized friction heat, no melting |
| Cycle time | Slow, includes flux and cooling | Fast | Typically 0.5–2.0 seconds |
| Consumables | Solder, flux, tips | Terminals, dies | None except sonotrode wear |
| Environmental | Flux fumes, lead-free compliance | Terminals add weight and cost | Flux-free, RoHS-friendly, clean |
For demanding applications such as automotive wire harness welding, the combination of low electrical resistance and high fatigue strength makes ultrasonic splicing the clear winner. Crimping remains cost-effective for low-current signal lines, while soldering is increasingly restricted to rework and repair environments.
Where Ultrasonic Splicing Delivers the Most Value
Ultrasonic splice welders are not a universal replacement for every crimp or solder joint. They shine in three categories of buyer demand:
- High-current power paths: Battery cables, starter/alternator circuits and inverter busbars benefit from the low joint resistance of a welded splice.
- Vibration-critical assemblies: Engine-bay harnesses, suspension sensors and commercial vehicle fleets experience constant shock. Ultrasonic joints do not loosen like crimps or fracture like solder.
- Mixed-material designs: Modern harnesses combine copper and aluminum to save weight. Borude ultrasonic metal welders create reliable battery tab welding-quality joints between dissimilar conductors without intermetallic embrittlement.

Borude BRD-7A terminal welder for high-current wire and busbar connections
What to Evaluate When Buying an Ultrasonic Splice Welder
When requesting quotations from ultrasonic welding machine suppliers, ask for these specifications and capabilities:
- Conductor range: Ensure the machine covers your smallest signal wire up to your largest power cable cross-section.
- Power and frequency stability: Look for automatic frequency tracking and overload protection to maintain weld quality across batch variations.
- Process monitoring: Models with weld-by-weld energy, amplitude and displacement logging support ISO/TS 16949 traceability requirements.
- Tooling life: Sonotrode and anvil life affect cost per joint; ask for documented cycle counts and spare-part lead times.
- Integration support: A good supplier provides mounting patterns, I/O maps and MES-ready data interfaces.
Borude supports buyers with sample welding reports, on-site or remote commissioning, and optional ultrasonic terminal welder configurations for combined splice-and-terminal applications.

Borude ultrasonic welding applications across automotive, refrigeration and energy storage
Why Borude Is the Right Partner
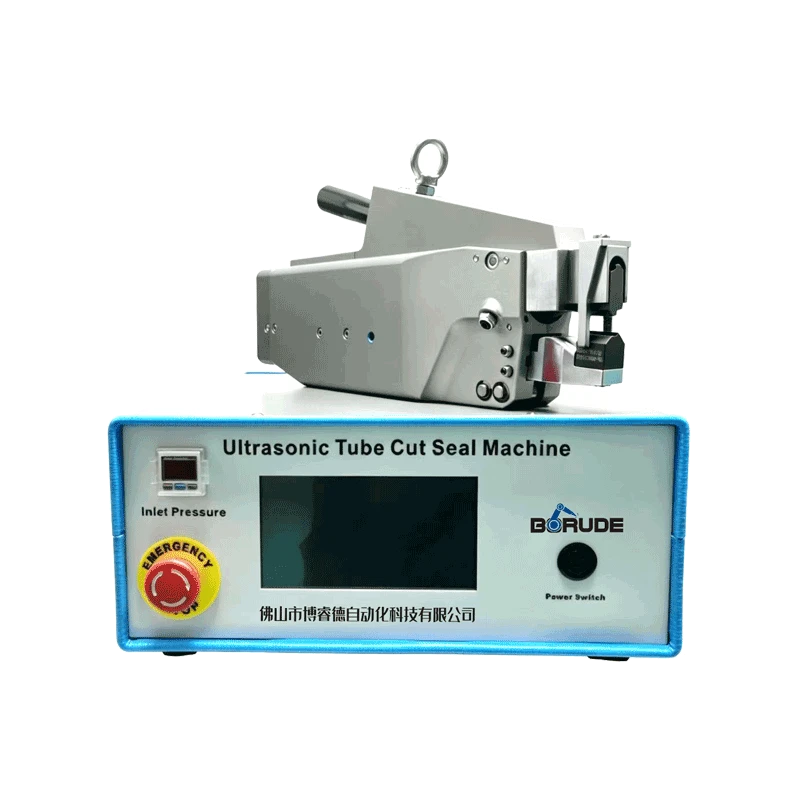
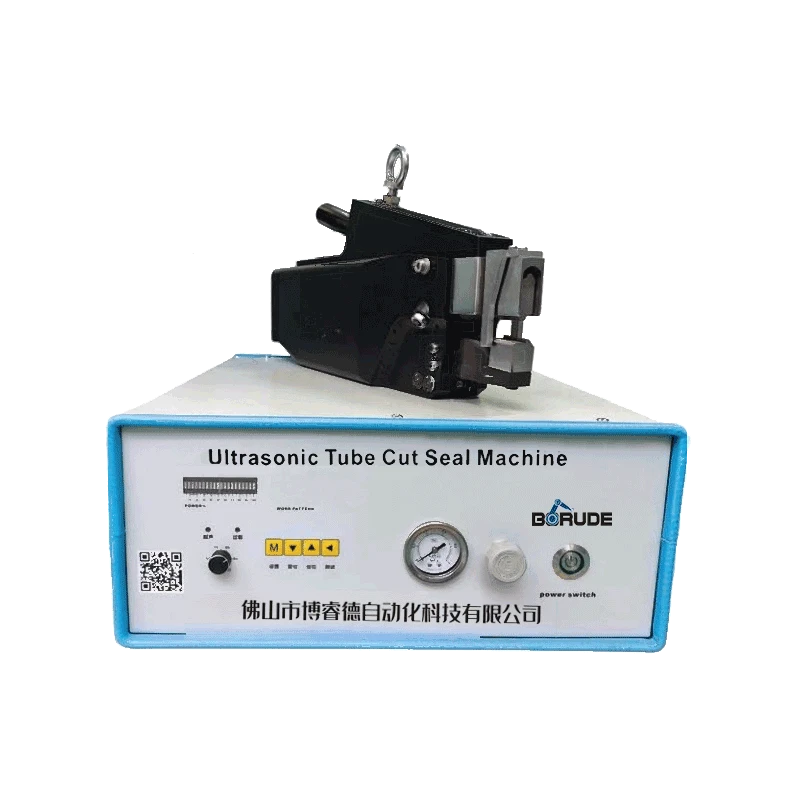
Borude specializes in ultrasonic metal welding and copper tube sealing equipment for export-oriented manufacturers. Our ultrasonic wire splicers are built with rigid frames, precision ultrasonic generators and quick-change tooling to keep your line running. We validate every application with pull-test and cross-section data before shipment, so you can release production with confidence.
Whether you are upgrading an existing crimp line or designing a new EV battery harness station, Borude provides application engineering, fixture design and after-sales spare parts from our Foshan headquarters.
Ready to replace solder and crimp with a stronger, cleaner joint?
Send your wire samples and production targets to Borude for a free weld feasibility report and quotation.
Contact Borude Today© 2026 Borude Sonic Equipment. All rights reserved. Ultrasonic wire splice welding, copper tube sealing and terminal welding solutions from Foshan, China.


